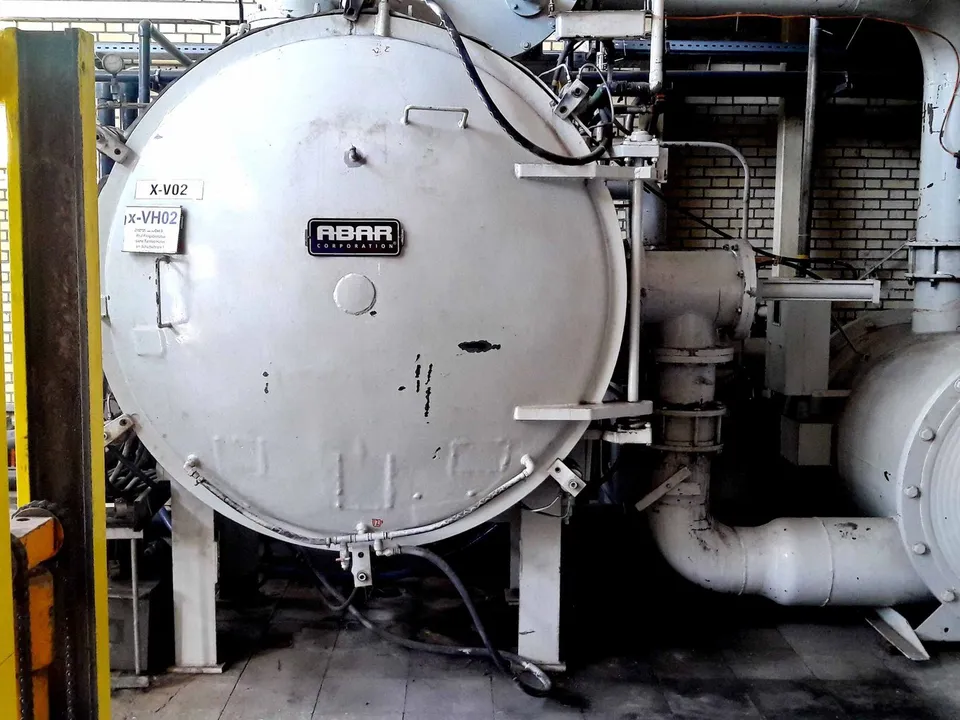
Vacuum heat treatment
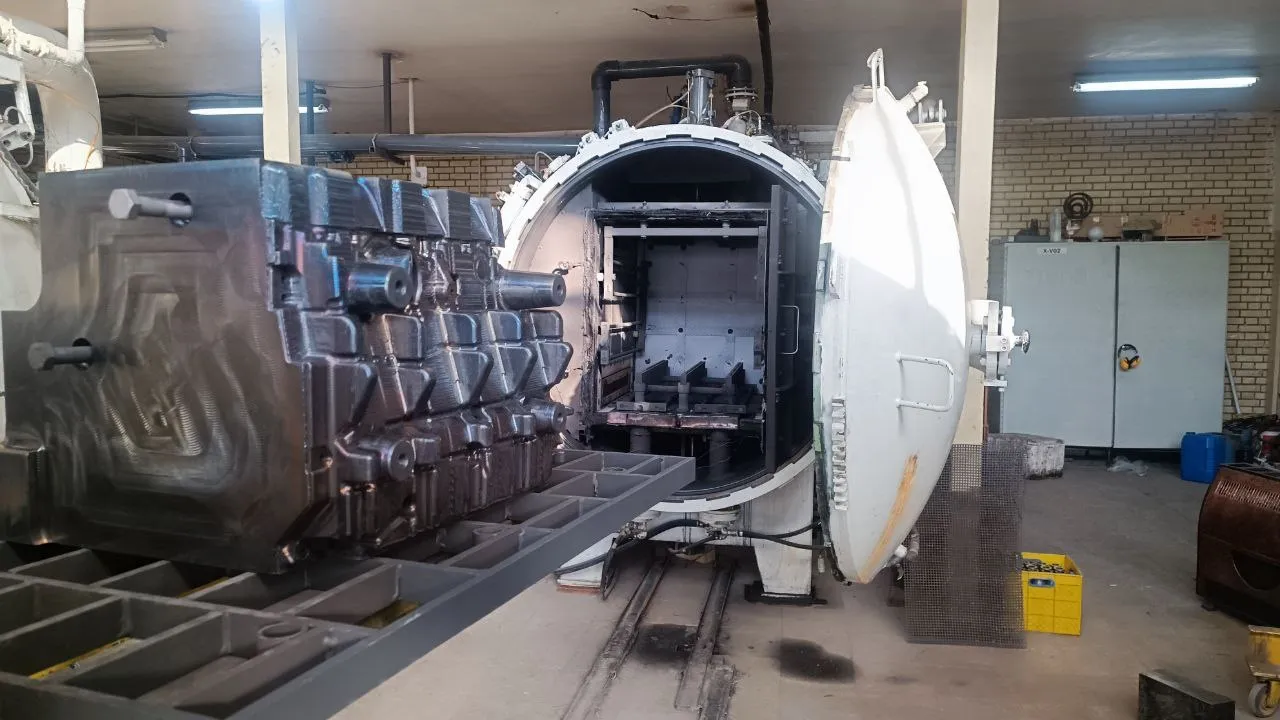
Hardening and tempering of tool steels and dies, and solution treatment and ageing of nickel superalloys.

Heat treatment · Tool steels and copper alloys
Controlled-atmosphere and vacuum furnaces, a metallurgy lab and technical consulting, operating around the clock in Tabriz.
We bring heat-treatment services, and the supply of tool steels and engineering alloys, to the region's industry. We see metallurgical advice as an inseparable part of our work, and we record the inspection results of every job for traceability.
Hardening and tempering of tool steels and dies, and solution treatment and ageing of nickel superalloys.
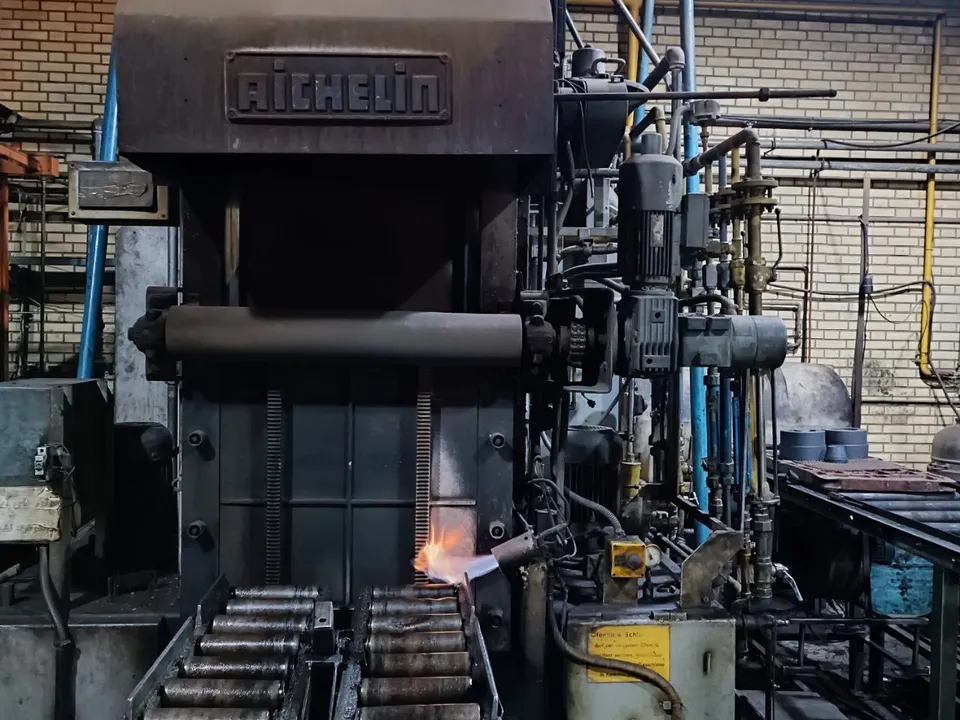
Gas carburizing, hardening, normalizing and annealing of parts such as gears and shafts.
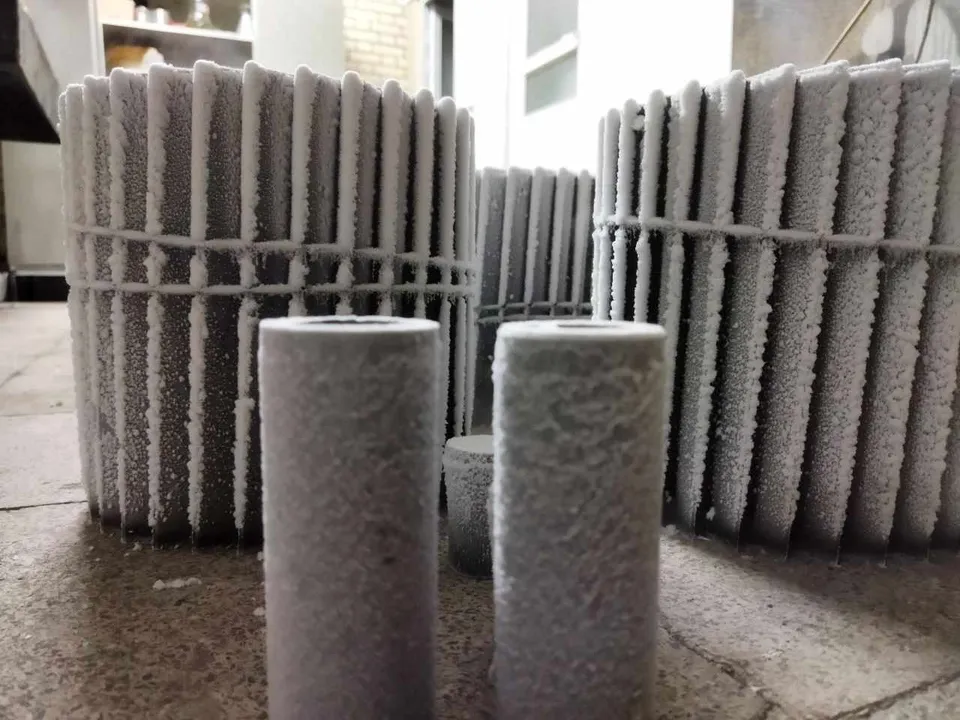
Transforming retained austenite into martensite, for more uniform hardness and dimensional stability.
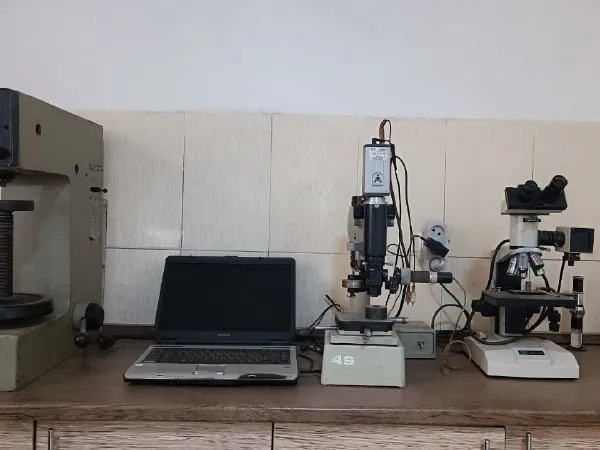
Hardness testing, metallography and case-depth measurement, also as a stand-alone service.
Shot blasting, technical consulting and steel and alloy supply are on our services page.
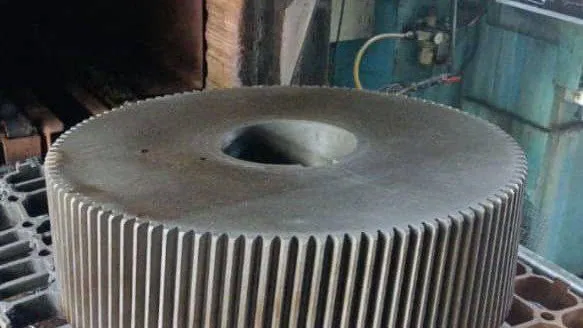
The gear's large section, and the temperature difference between its surface and core during heating and quenching, make its heat treatment very sensitive. Cracks are far more likely to start and grow in a part like this than in an automotive gearbox gear.
So the temperature was raised in steps, at 450 °C, 800 °C and 860 °C, and finally to 920 °C. The oil temperature and quench time were chosen with care, and after hardening the gear was tempered twice.
See more on our projects page.
Automotive, tool and die making, oil, gas and petrochemicals, steel and refractories, power generation and special industries. See what we do for each on our industries page.
Tell our specialists the material, size and hardness your part needs, and we will recommend the right process.
Parts reception and delivery: daily, 8:00–20:00